Mining Pump | 50HP
SKU:
HTSVECMNP0000052
₦17,000,000.00
Why customers choose us
- Satisfaction Guaranteed
- Fast delivery
- Secure Payments
- 24/7 Customer assistance
Other people want this. 4 people have this in their carts right now.
A Mining Pump | 50HP is a robust and powerful pump specifically designed to handle the demanding conditions encountered in mining operations. These pumps are engineered to move water, slurry, and other fluids containing abrasive solids, making them essential for maintaining operational efficiency in mines.
Key Features of Mining Pump | 50HP:
- Engine Power:
- The pump is driven by a 50 HP motor, providing a balance between power and efficiency.
- Flow Rate:
- Depending on the model, the pump can deliver a flow rate of 150,000 to 400,000 liters per hour.
- Head Lift:
- Capable of achieving a head lift of up to 80-100 meters, this pump can efficiently move fluids vertically, making it ideal for deep mining applications.
- Construction:
- Constructed from high-strength materials like cast iron, stainless steel, or specialized alloys to resist wear and corrosion caused by abrasive slurries and harsh mining environments.
- Abrasive Handling:
- Designed to handle slurries containing sand, gravel, or other solids, with features such as replaceable wear parts and open impellers that minimize clogging.
- Drive Type:
- Available in both electric and diesel-powered versions, providing flexibility depending on the power availability at the mining site.
- Portability:
- Some models come with skid or trailer mounts for easy transportation and deployment across different sections of the mine.
Applications of Mining Pump | 50HP:
- Dewatering: Used to remove water from mine shafts, tunnels, and pits, ensuring safe and dry working conditions.
- Slurry Transport: Capable of pumping slurry mixtures containing rock, sand, and other solids.
- Mud Handling: Effective in removing mud and sediment from excavation sites or tailings ponds.
- Emergency Flood Control: Deployed to manage sudden flooding in mines, preventing damage and downtime.
Advantages:
- Reliability: Built for continuous operation in harsh conditions, reducing the risk of downtime.
- Durability: Designed with materials and components that withstand wear and tear from abrasive slurries.
- Efficiency: Balances power consumption with performance, ensuring effective operation without excessive energy costs.
- Versatility: Can handle a wide range of materials and conditions typical in mining environments.
Considerations:
- Maintenance: Regular inspection and maintenance are critical to avoid wear-related failures.
- Energy Consumption: Operating a 50 HP motor can be energy-intensive, so efficiency should be considered when selecting a model.
- Initial Cost: The robust construction and capabilities of these pumps typically come with a higher initial cost, making them a significant investment.
A 50 HP Mining Pump is ideal for operations requiring consistent, reliable performance under challenging conditions. If you need further information on specific models, compatibility with your mining site, or procurement options, let me know!
Additional information
| Weight | 1700 kg |
|---|
Only logged in customers who have purchased this product may leave a review.
Related products
Temperature and Humidity Monitors are invaluable tools for maintaining optimal environmental conditions in various applications, including incubators, climate-controlled rooms, storage facilities, and agricultural settings. Regular calibration, proper placement, and regular maintenance are essential for ensuring accurate and reliable measurements.
A quality LCD temperature and humidity meter with a full range of functions and class-leading accuracy.
OUT OF STOCK
Advantages compared with the old incubator:
1.This is an updated version of the incubator, there are two functions of the incubator: hatcher, brooder. So you don't need an additional hatcher.
2. Space increased, this is good for the airflow in the equipment, make the temperature more uniform, enhance the hatching rate.
3.Because of the hatching basket protection, the machine avoids the death of a newborn chick when it falls off the egg tray and cannot be taken out in time.
4.The chicks can stay in the machine for a long time, so the chicks will be more healthy and increase the survival rate.
Chicken Drinker | 10L are made of plastic, metal, or other materials, and their design often depends on factors such as the number of chickens, the setup of the coop or farm, and the preferences of the farmer. The primary purpose of a chicken drinker is to ensure that chickens have a continuous supply of clean water to meet their hydration needs.
3 Tier Local Battery Cage (96 Birds per Unit)
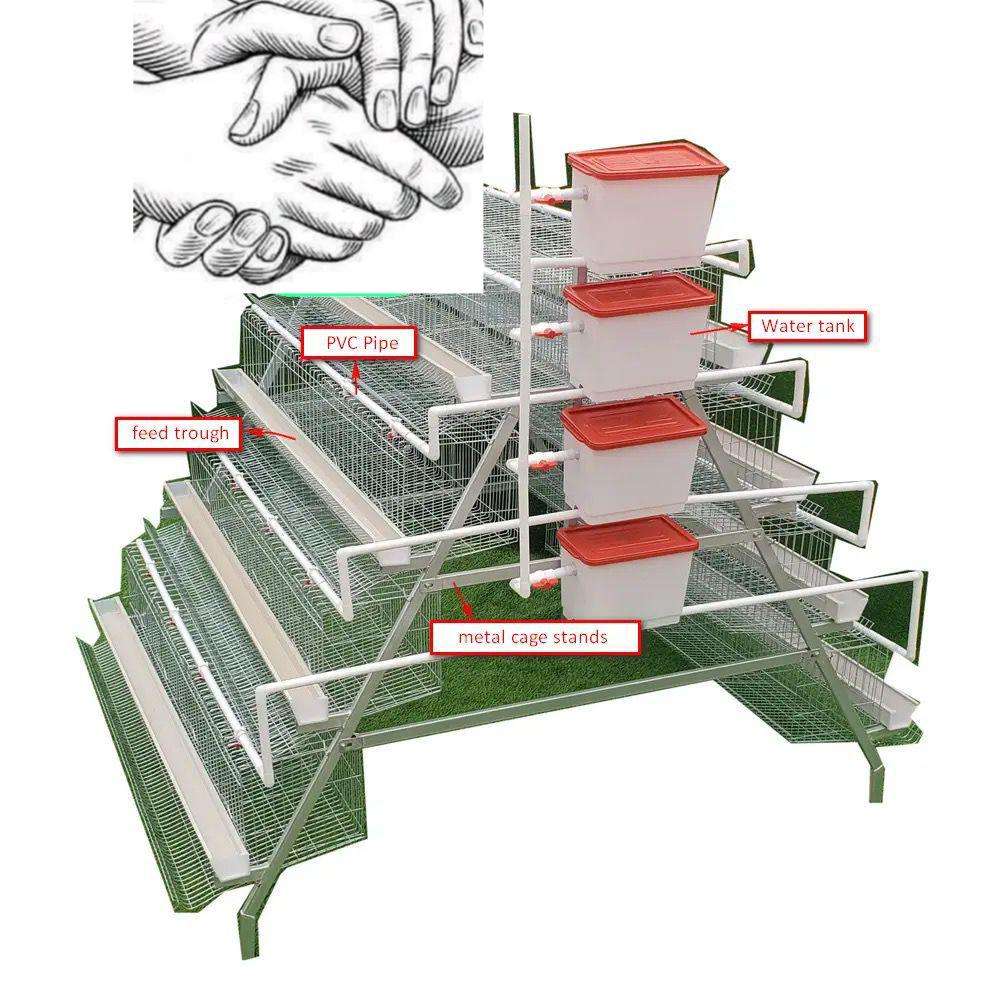
A galvanized battery cage system for 126 birds per unit offers a practical and efficient solution for poultry farmers looking to maximize space, improve egg production, and streamline farm management. With proper installation, maintenance, and adherence to welfare standards, this system can contribute significantly to the success and profitability of a poultry farming operation.
Lifespan: 7 - 10years
Recommended for small processing units with low capacity, our range of manual evisceration tools can be very useful to help you eviscerate poultry. Poultry shears will allow you to cut poultry feet and wings.


Reviews
There are no reviews yet.